Counted,
Then Ahead
After Capture
Measured data leads to line status, output forecasts and staff reallocation suggestions.
Three Stages After Capture: Real-Time View, Output Forecast, Preventive Action
RTP · TV Kanban
Predicted Output · Operation Simulation
Line Balancing · Auto Layout
One grid cell is one workstation; bar length is output today. Bottleneck position and reallocation direction are illustrative examples.
From Seconds
to Seasons
Seconds to Seasons
Time measured every cycle accumulates into the factory SMV and becomes the basis of Monolis costing.
From One Measured Cycle to Factory SMV to Costing Standard
- 1
1 CYCLE One Sewing Cycle
The workstation meter logs count, sewing and handling time per cycle.
- 2
1 DAY One Day
Line output and % of target accumulate by the day.
- 3
1 WEEK One Week
AMV per operation is grouped by style and line.
- 4
PROFILE Operator · Operation Profile
Operator skill and operation performance trends become profiles.
- 5
STANDARD Factory SMV
Outliers are removed and operation standards are set.
- 6
COST Monolis Operations · Labor
The set values become the basis of Monolis Operations · Labor.
See how SMV leads to cost on the Monolis page. Monolis Operations · Labor
Two Builds,
One Standard
Device Ver. · Tablet Ver.
Two configurations chosen by factory size and operating style. Either way, data accumulates on the same standard.
Device Ver. for Mass Production, Tablet Ver. for High-Mix Low-Volume
Device Ver.MONOLOG V1 | Tablet Ver.MONOLOG V2 | |
|---|---|---|
| Setup · Measuring | ||
| Components | Smart counter · Pedal angle gauge · Andon | Industrial tablet · Pedal angle gauge · Andon |
| Principle | Sewing span from machine vibration, pedal angle | Hand coordinates, pedal angle split sewing and handling |
| Data Collected | Cycle count · Sewing time · Handling time | Cycle time · Hourly output · Joint coordinates · Sewing motion |
| Operator Input | One button press per piece | ID · QR login, then pick operation |
| Video · Privacy | No personal data taken | No video stored, joint coordinates only |
| Specs · Certs | ||
| Unit | Counter with vibration sensor and count button | 10-in industrial tablet |
| Camera | None | Built-in camera |
| Pedal Sensor | Pedal angle gauge (bracket on pedal plate side) | Pedal angle gauge (bracket on pedal plate side) |
| Compute | Signals sent to the zone computer | Processed on tablet; only results sent |
| Network · Storage | Wi-Fi; held on zone computer if link drops | Encrypted Wi-Fi; held on tablet if link drops |
| Power · Install | 1 set per machine, any sewing machine brand | Power per cell, about 2 min install per cell |
| Andon | 10-step lamp shows progress vs target (on workstation) | Same Andon, on the right thread stand |
| Certs · Tests | FCC · QCVN 18 · QCVN 112 · IP4X | IP65 · MIL-STD-810H (1.2 m drop) |
| Where It Fits | ||
| Line Type | Mass line, many workstations | High-mix line, frequent style changes |
| Control Mode | Central control: production control team manages all lines | Cell control: operators select and manage operations per cell |
Field
to Screen
Structure
Values measured at the workstation reach the screen through the zone computer and cloud.
Edge Collection Continues Without Internet, Auto Transfer on Recovery
If the internet drops, edge collection continues; when it returns, queued records upload to the cloud in order.
EVENT LOG · ZONE 03
- 08:12Workstation 07 · 1 piece doneZone computer save → cloud transfer
- 08:13Workstation 12 · 1 piece doneZone computer save → cloud transfer
- 10:41Internet link lostZone computer starts holding records
- 10:42Workstation 07 · 1 piece doneSaved on zone computer · queued
- 11:30Workstation 12 · 1 piece doneSaved on zone computer · queued
- 12:05Internet restoredHeld records sent in order
- 12:06Queued records sentStatus board · web updated
DATA TIMELINE
Times and events are examples for illustration.
Built for
the Line
Factory Setup · Ops
The equipment installed from workstation to screen, plus rollout and operation.
Security on OPC-UA · AAS Standards and Mutual Authentication, Edge to External Use
The zone computer acts as the OPC-UA gateway, converting MQTT · Modbus · REST signals into OPC-UA variables, and communication on this path is protected by signing, encryption and X.509 mutual authentication.
AAS organizes master data, Lot tracking, BOM and carbon footprint (PCF) data in the DB into 7 official IDTA Submodels,
served via a standard API for the EU Digital Product Passport (DPP), carbon border adjustment (CBAM) evidence and buyer audits.OPC-UA covers the entire collection path, protected by signing, encryption and X.509 mutual authentication. AAS organizes Lot tracking · BOM · product carbon footprint (PCF) data into 7 official IDTA Submodels and provides them through a standard API.
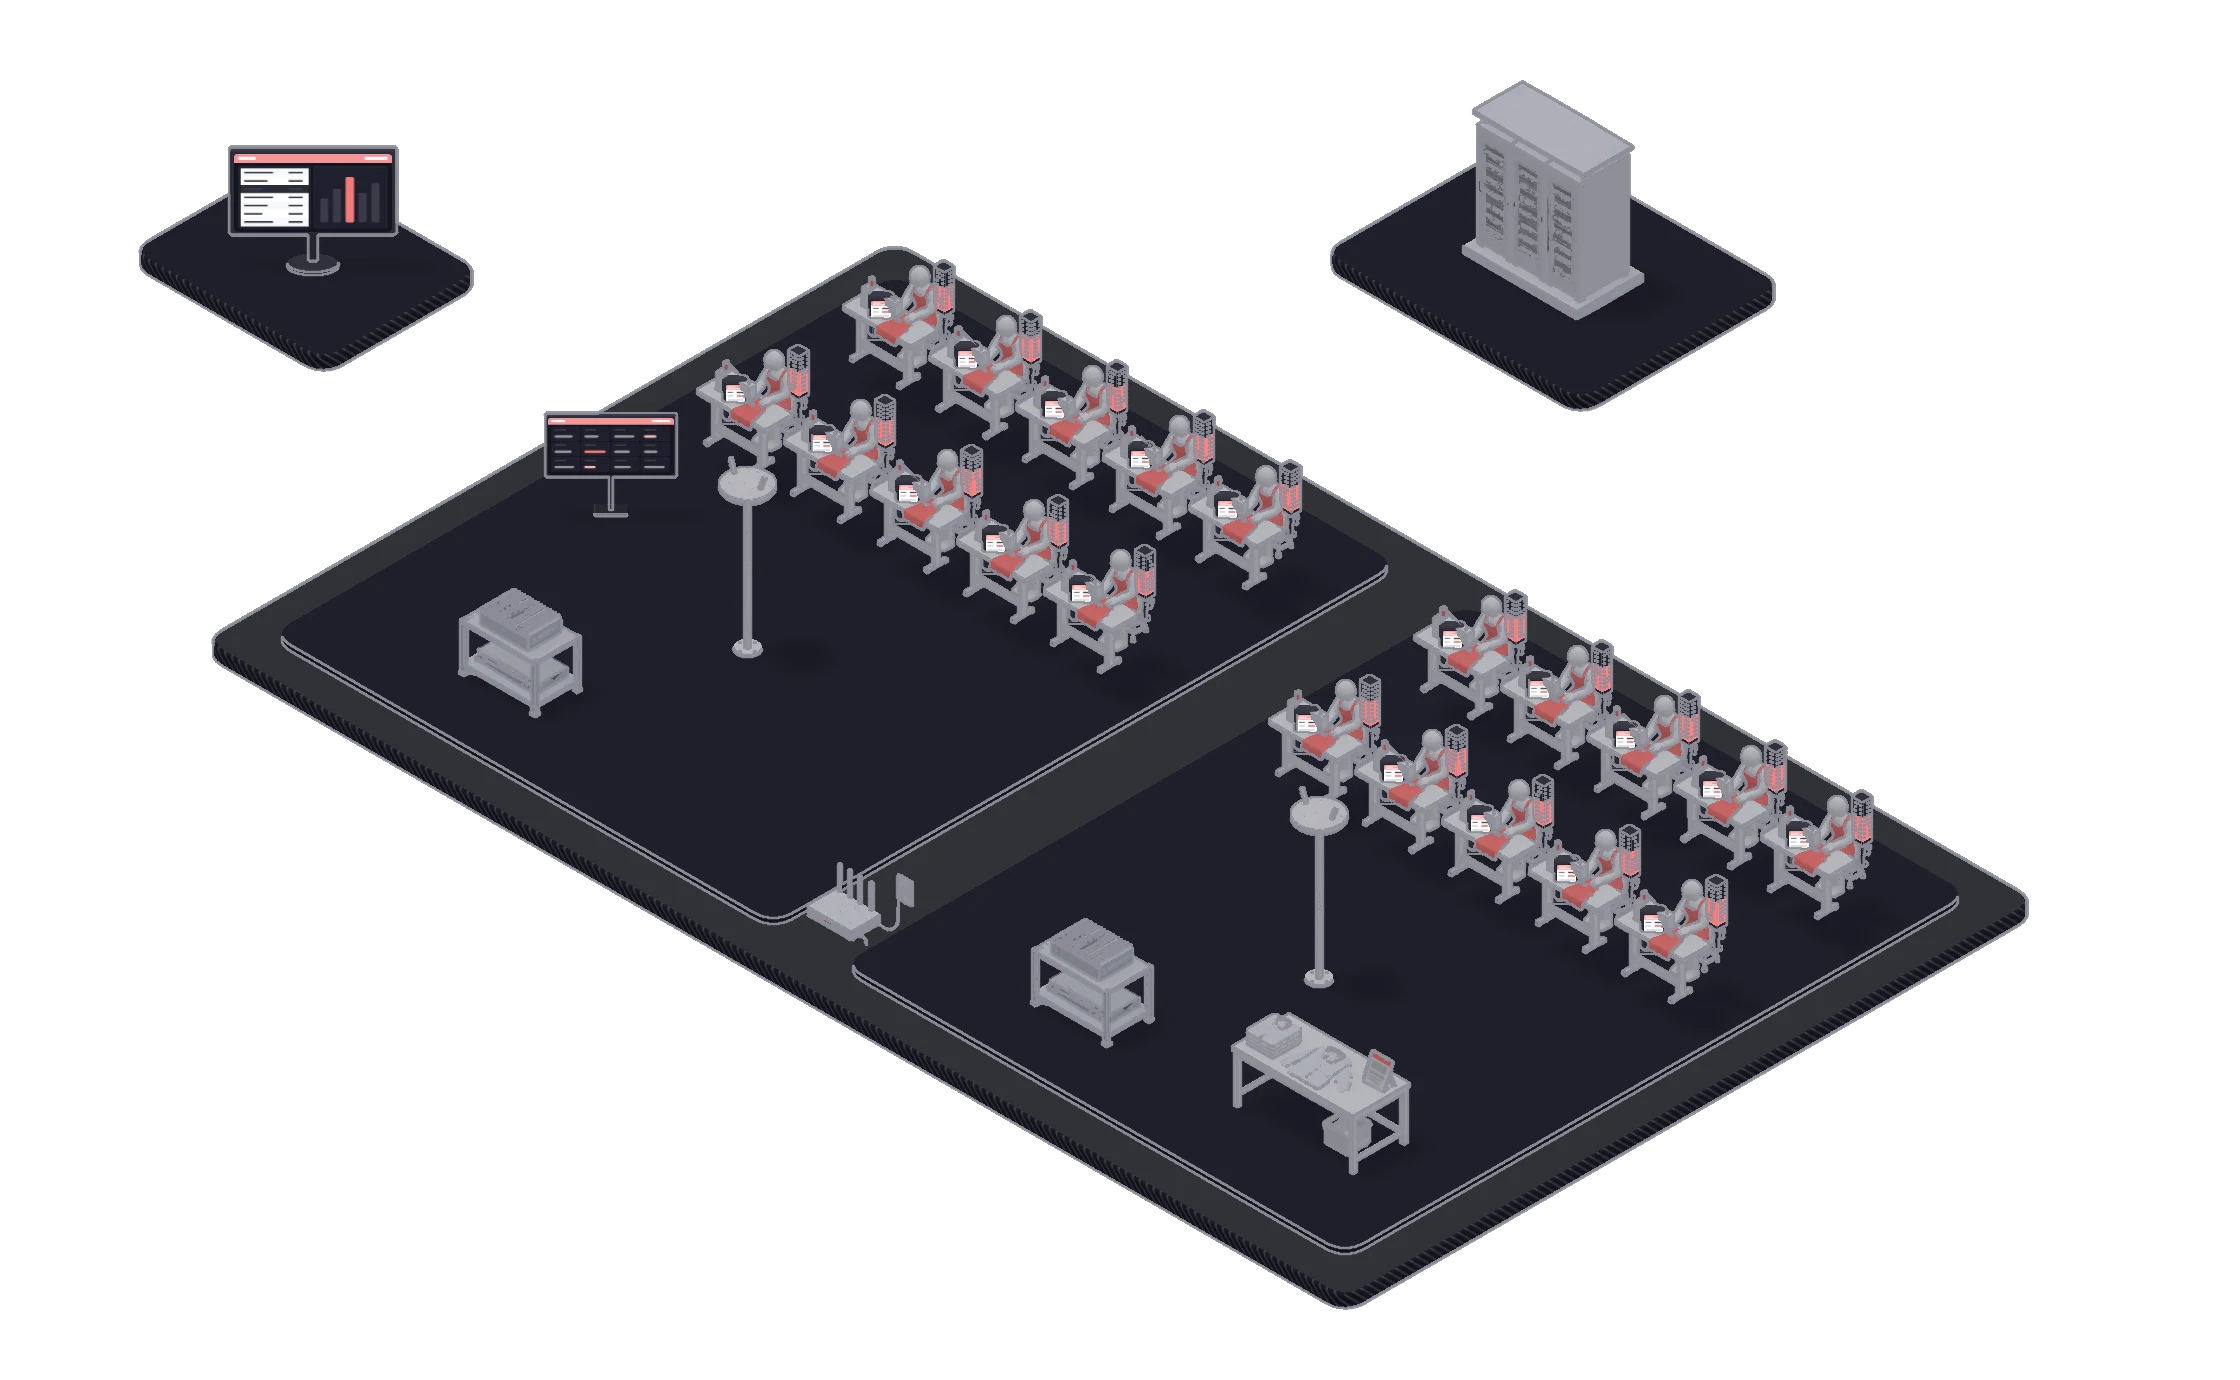
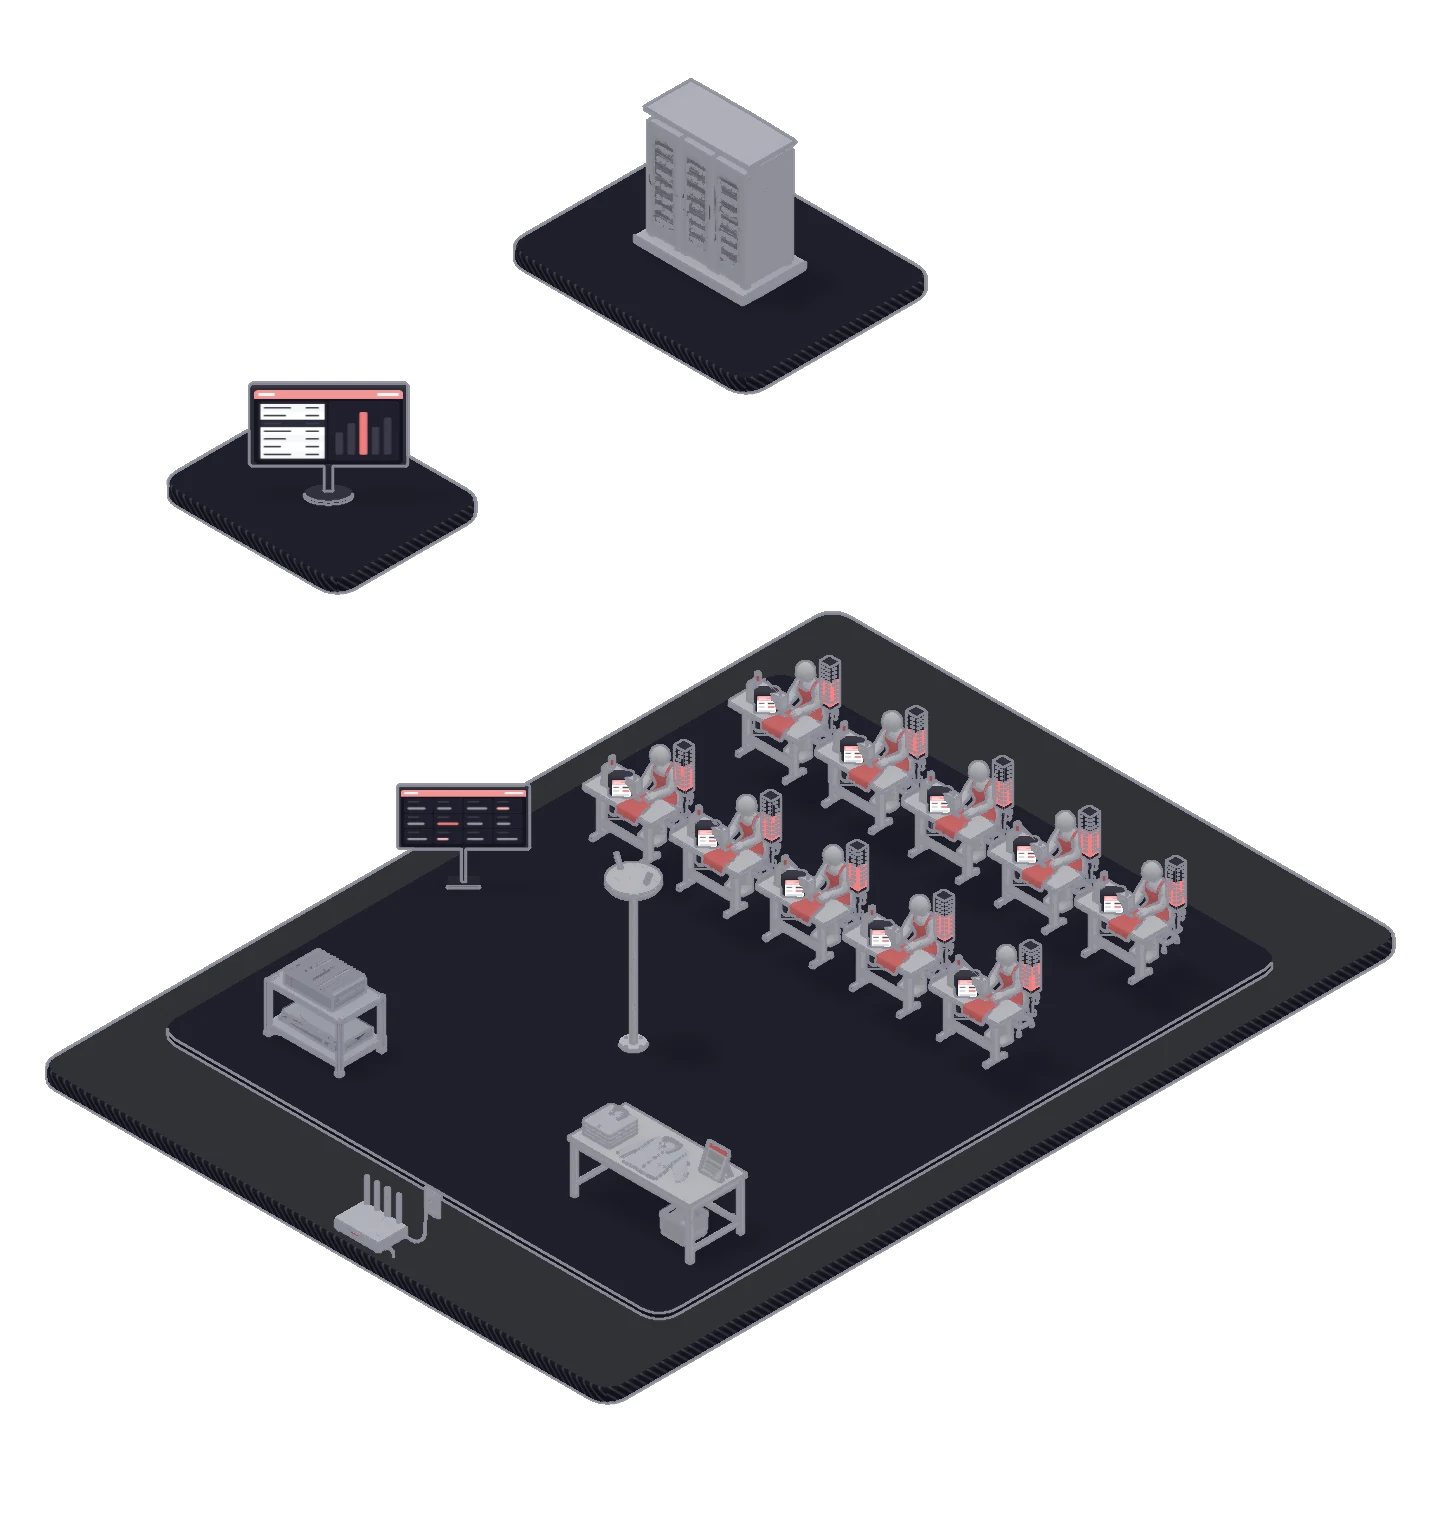
The example shows 2 zones of 2 lines each.The example shows 1 zone of 2 lines. Numbers in the diagram match the numbers in the table below.
| 1Meter | 1 set per sewing machine (Device Ver. or Tablet Ver.) |
| 2Wi-Fi Router | 1-2 per line, installed about 2 m above the floor |
| 3Zone Computer | 1 per 1-2 lines, stores records inside the factory first |
| 4Internet Gateway | Links zone network and internet |
| 5SIJE Cloud | Turns records into operation standards and output |
| 6Screens | Line status board TV · Web dashboard · QC tablet |
| Internet Down | Collection continues; backlog auto-sends on recovery |
| Zone Isolation | A fault in one zone does not affect other zones |
| Monolis | Receives line standards, sends AMV and output |
| QC | Finished goods inspection logged on QC tablet |
| Rollout | SIJE handles network setup through line setup |
| Warm-Up Period | 3 days of data after install, then forecast · reallocation |
| Hardware Scope | Split: SIJE-supplied · locally sourced · customer-provided |
| Comm Standard | IEC 62541 OPC-UA(OPC UA for ISA-95) |
| Comm Security | Basic256Sha256 signing · encryption, X.509 mutual auth |
| Data Standard | IEC 63278 AAS, 7 official IDTA Submodels |